ISO 3834-2 welding requirements cover the manufacturer’s controls for fusion welding of metallic materials, from reviewing the job to keeping quality records. They link procedures, competent persons, and suitable equipment and inspection. For the buyers the right question is whether those controls cover the activities being ordered.
Updated October 2026
A fabrication certificate, a welder’s qualification and a machine specification each answer a different question. Confusing the three can lead to an impressive purchase order, but no means to accept the finished product. This guide clarifies the differences and provides tools to enable quality, production and procurement personnel to perform verification/inspection.
ISO 3834-2 welding requirements at a glance
ISO 3834-2 sets the comprehensive quality requirements for fusion welding of metallic materials in workshops and at field installation sites. A manufacturer needs control over the activities that influence welding quality, including technical review, personnel, procedures, equipment, materials, inspection and records. The focus is on manufacturing operations, rather than on a single machine.
El International Organization for Standardization’s Part 2 scope establishes that boundary. “Comprehensive” is the name of the requirement level, not an assurance that a supplier is capable of welding every material or product.
Think of requirements for fusion welding as a connected control system. Prior to production, determine the applicable specification and capability to satisfy it. During the work, employ correct instructions, qualified personnel and controlled equipment. Prior to release, confirm that the inspection results and quality records show what was performed.
For a buyer assessing vessel fabrication, start with the work specified in the purchase order. A manufacturer certificate is useful but doesn’t specify an acceptance criterion for each weld. Include that in the job specification, along with the relevant product standard and required documentation.
ISO 3834-1: choosing the right quality level
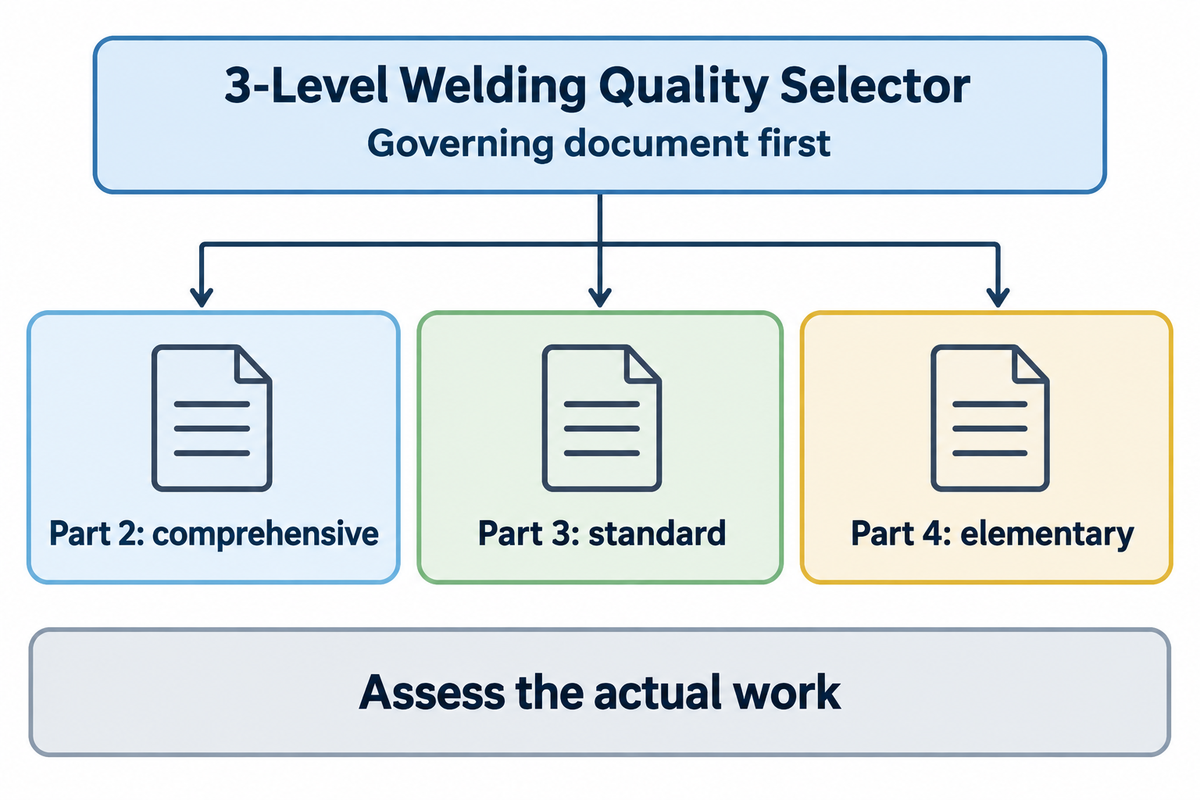
Part 1 gives the basis for choosing comprehensive, standard or elementary welding quality requirements. Start with any level already stipulated by the product standard, regulation, or contract. If options are unrestricted, give priority to complexity of work, the kind of materials and the consequences of failure. A sector label doesn’t determine selection.
3-Level Welding Quality Selector
The table supports a selection discussion with the responsible welding and quality personnel. First note the requirement governing the selection; then identify the technical evidence for the proposed level.
| Level | Selection discussion | Evidence to bring |
|---|---|---|
| Part 2: comprehensive | Required by the governing document, or justified by demanding safety, material or fabrication conditions. | Specified level, product risk, material range and fabrication complexity. |
| Part 3: standard | Evaluate standard quality requirements against the actual application where the level is not already prescribed. | Service conditions, known weldability and established production methods. |
| Part 4: elementary | Consider elementary requirements only where the governing requirements and technical assessment support them. | Safety significance, loading conditions and reasons the proposed controls are sufficient. |
Selection factors summarized from ISO 3834-1 y ISO 3834-6 implementation guidance; the table is a buyer’s discussion aid.
Hypothetical example: A workshop receives enquiries for a simple support frame and a dynamically loaded tower section. Procurement proposes a single requirement level for both, as both are made of steel. The quality manager, however, differentiates the orders, checks their governing specifications, and captures the material, design and fabrication factors for each. If the tower section contract states it should be in accordance with Part 2, that would govern the order. The other order gets assessed on its own. The important outcome is documented selection for each manufacturing scope, with the reasoning evident to sales and production. Buying a more capable machine won’t resolve that selection, and it doesn’t change the customer’s contractual requirement.
ISO 9001 welding quality requirements and ISO 3834
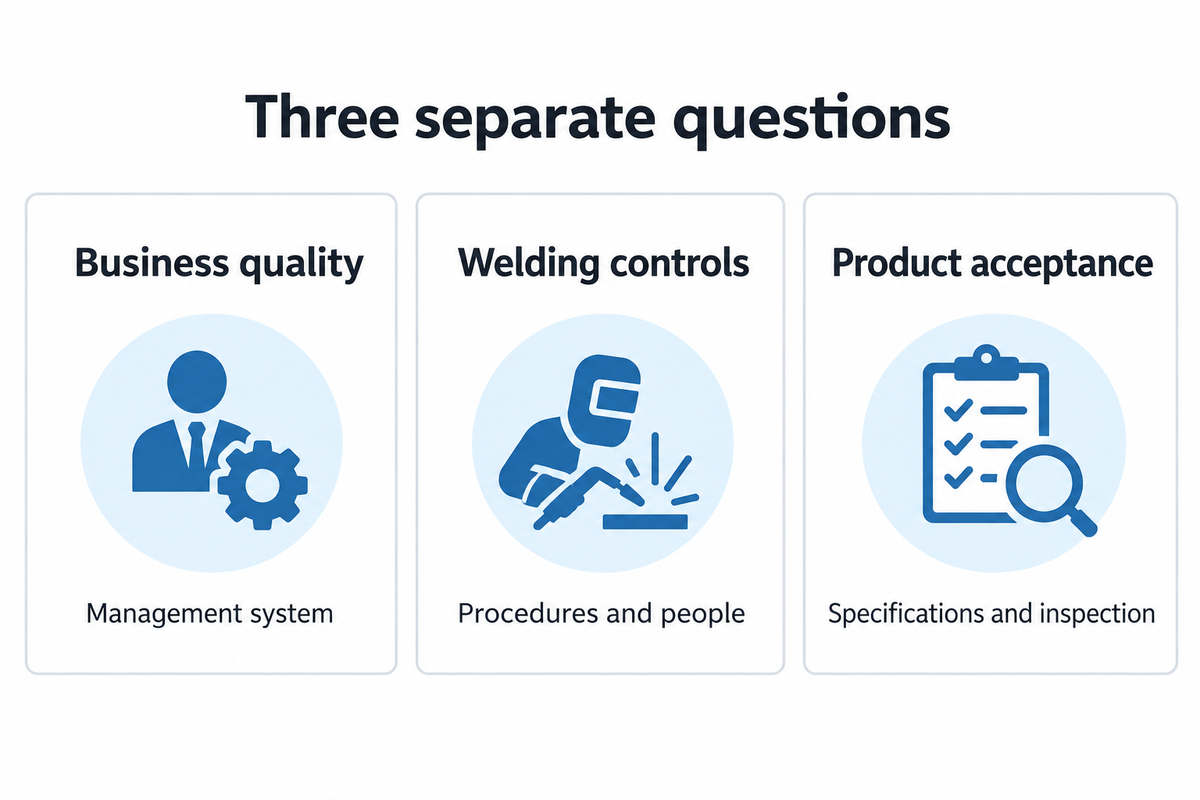
ISO 9001 addresses the quality management system across an organisation; ISO 3834 addresses welding-specific quality controls. Within the welding industry, the standards can work together, and ISO 3834 can also be used independently. Therefore, a general quality-management system certificate does not, on its own, demonstrate compliance with the welding requirements of a given contract.
Keep three questions separate: How does the business manage quality? How does it control welding? And how will the welded product be accepted? The first question looks at the management system. The second question considers procedures, personnel and production controls. The third question looks at the applicable product specifications, inspection plan and acceptance criteria.
When a supplier sends an ISO 9001 certificate in response to an ISO 3834 request, ask for the welding-specific evidence associated with the quoted scope. This makes the document review more useful than just collecting certificates. Record the entity, site and work covered by each document to avoid confusion due to similar company names or different facilities.
ISO 3834 welding procedure specifications and qualified people
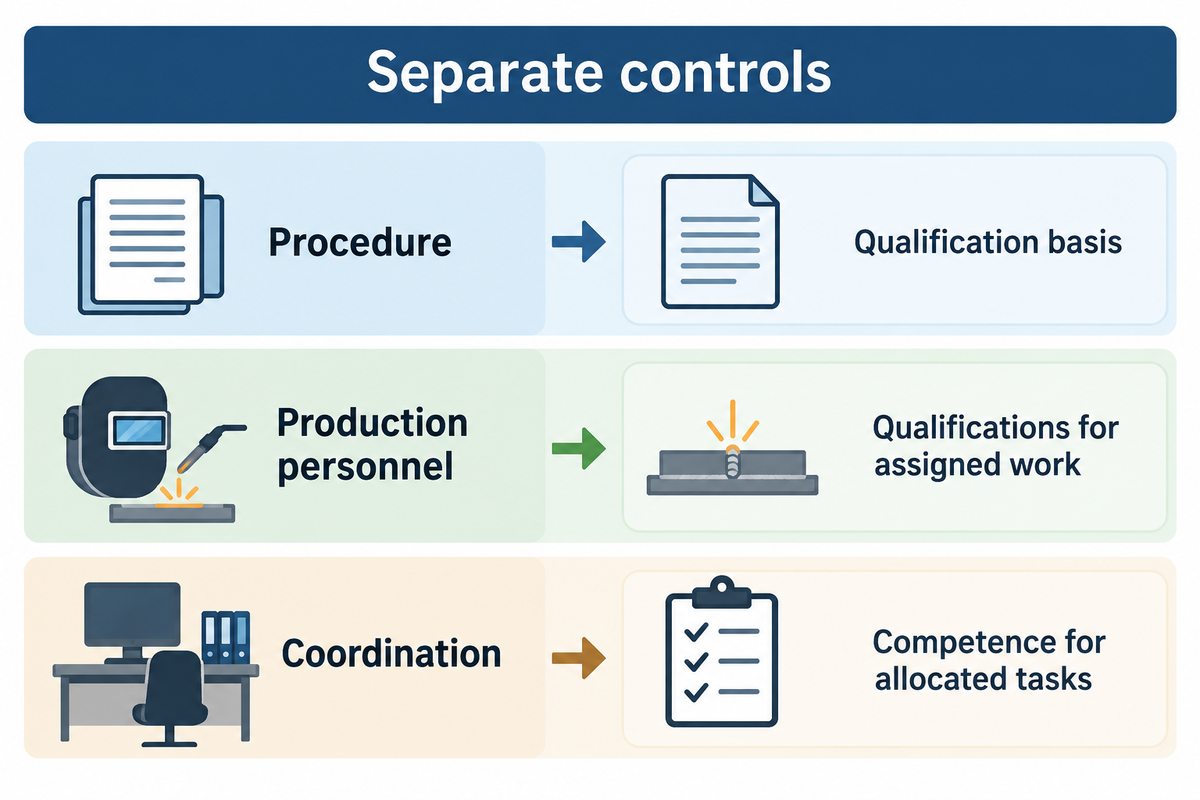
Welding procedure specifications define how welding is performed. Their qualification basis, the qualifications of the personnel doing the welding and the competence of coordination personnel are separate controls. Match each to the actual process and manufacturing scope before releasing the work to production.
What are welding procedure specifications?
A welding procedure specification, or WPS, defines a welding operation. The manufacturer links that definition to the qualification basis. The correct revision is made available where it’s used. A qualification record is supplementary; it doesn’t replace the production instruction.
ISO 3834-5:2021 identifies the international standards and relevant provisions for claiming conformity to Parts 2, 3 or 4. Use that document with the applicable product requirements when establishing the procedure and personnel qualification route. A procedure copied from another job needs a scope check before use.
What qualification does a welder need?
A welder needs the qualifications pertinent to the assigned work under its governing standards and contractual requirements. Review the process, material and qualification range and don’t just accept the statement “qualified”; mechanized or automatic welding can involve a different personnel category, namely the welding operator or weld setter.
ISO 14732:2025 addresses operators and setters for mechanized and automatic welding within its stated scope. Its exclusions matter: a person merely handling a workpiece is not automatically performing the same role as someone controlling parameters or setting up the welding equipment.
ISO 14731 welding coordinator responsibilities
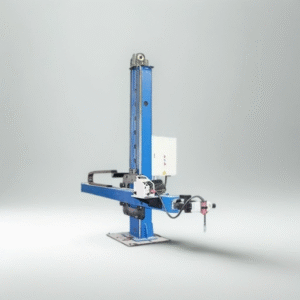
The coordinator’s job is different again. ISO 14731:2019 addresses welding-coordination tasks and competence for the responsibilities allocated. For a new production cell, identify who approves instructions, handles technical queries and evaluates changes. Training on the controls of a manipulador de soldadura supports operation, but does not establish all those responsibilities.
ISO 3834 equipment maintenance and production controls
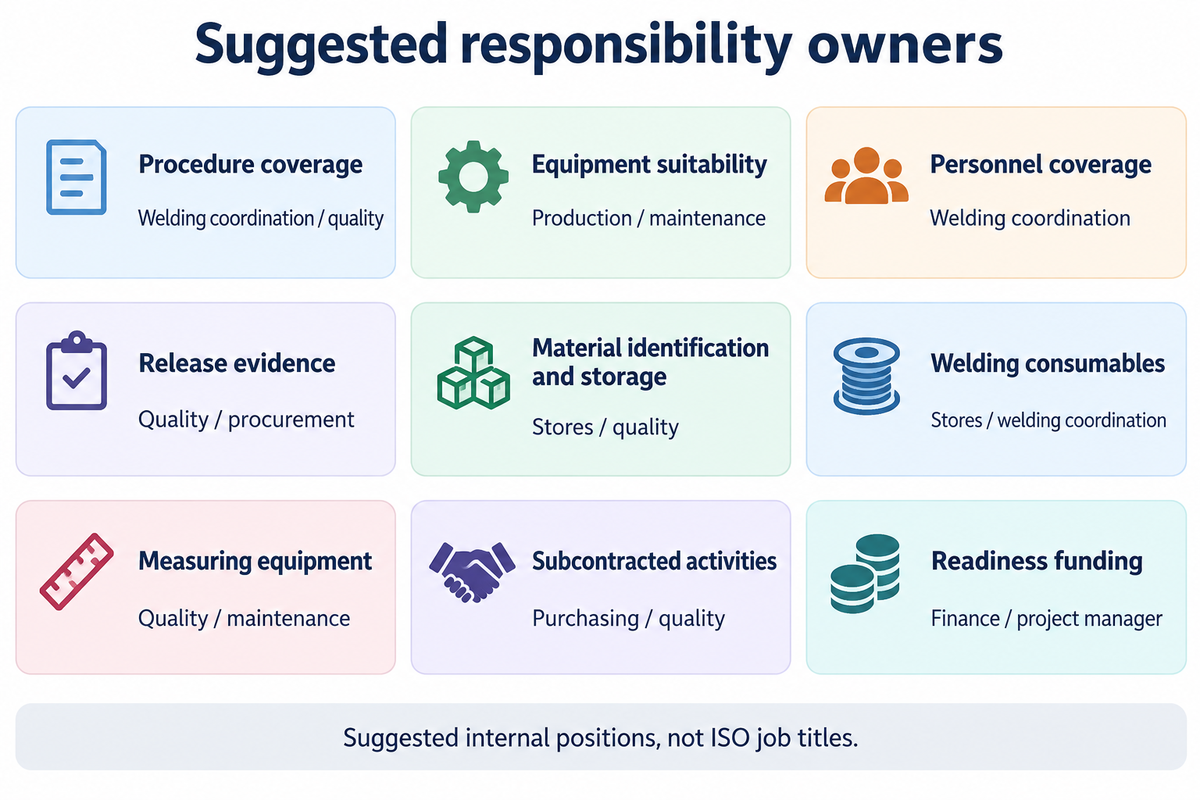
Equipment control refers to keeping equipment suitable for the work to be performed and managing the records, checks and maintenance that support its use. Welding quality relies on proper material identification, handling of consumables and controlled instructions. Outsourcing an activity creates a new interface that the manufacturer must manage.
Welding quality responsibility matrix
This division refines the broad request for compliance into work that can be assigned by the production, quality and purchasing teams. The roles shown are suggested internal positions, not job titles based on ISO.
| Control category | Suggested owner | Evidence needed | What remains unresolved without it |
|---|---|---|---|
| Procedure coverage | Welding coordination / quality | Applicable WPS and qualification basis | Whether the proposed production operation is covered |
| Equipment suitability | Production / maintenance | Job requirements, equipment capability and relevant condition checks | Whether the cell can carry out the approved work |
| Personnel coverage | Welding coordination | Task assignments, competence and applicable qualifications | Who is authorized and qualified for each task |
| Release evidence | Quality / procurement | Inspection records, traceability and resolved nonconformities | The basis for accepting the ordered work |
| Material identification and storage | Stores / quality | Material identification, storage arrangements and required traceability records | Whether the correct material reaches the assigned job |
| Welding consumables | Stores / welding coordination | Specified consumables and applicable handling instructions | Whether consumable selection and condition support the approved procedure |
| Measuring equipment | Quality / maintenance | Required checks and applicable calibration or validation records | Whether measurements used for acceptance have the required basis |
| Subcontracted activities | Purchasing / quality | Communicated job requirements and returned records | Whether outsourced work meets the agreed manufacturing requirements |
| Readiness funding | Finance / project manager | Separate preparation, qualification and assessment costs | Whether the budget funds the work needed before audit |
Editorial responsibility mapping based on TWI’s welding-quality control areas and ISO 14731.
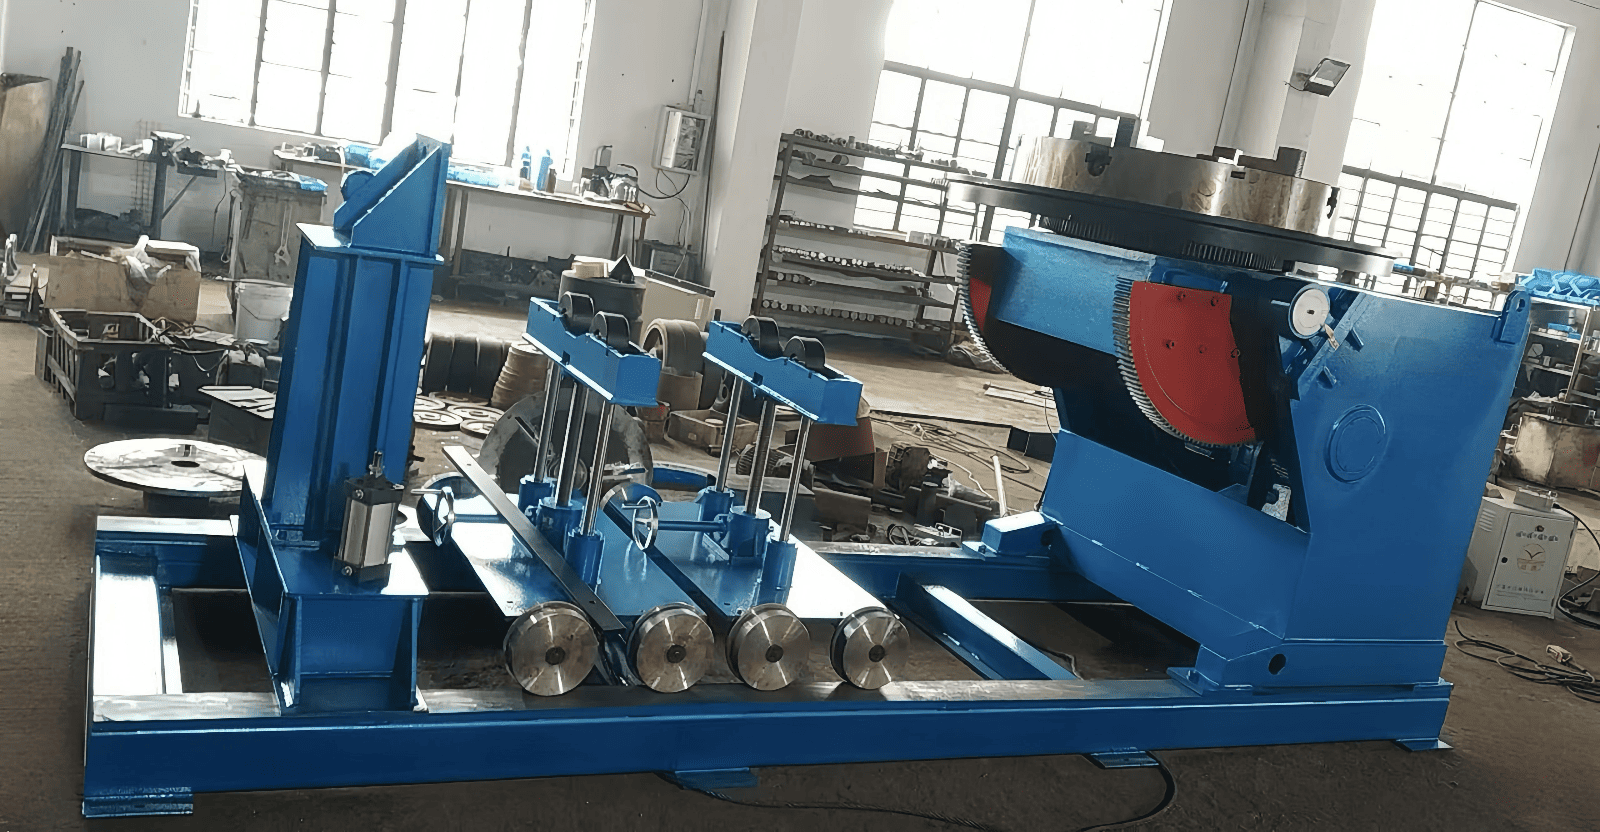
Hypothetical example: A plant has installed a positioner for a repeat fabrication job. Production has verified the load and clearance and the quality team has verified the procedure and assigned personnel. However, during handover it was found that no one owns responsibility for the equipment’s maintenance record and the current instruction at the workstation. The project manager assigns those tasks before routine production work begins. The fact that the work isn’t done is a control system issue and not a reason to assume the machine is unfit for use. Keep this handover distinct from choosing a welding positioner, where fixture loading, movement and access need their own assessment. A signed equipment purchase order doesn’t resolve either set of tasks.
ISO 3834 inspection and testing: quality records
Inspection and testing need a defined purpose, method and acceptance basis for the actual welded products. Link the inspection plan to the associated specification and keep the results traceable to the work. An ISO 3834 certificate cannot supply a universal test percentage or establish that every delivered weld has passed inspection.
“The quality of the weld is manufactured into the product, not inspected.”
Welding is a process whose final results can’t always be verified through testing. Treating welding as a special process places controls in the manufacturing process to support product quality. Therefore, procedure control and inspection go hand in hand. Destructive testing associated with qualification and inspection of production welds answer different questions and their records should be distinguishable in a work file.
Welding quality assurance plan: inspection and traceability
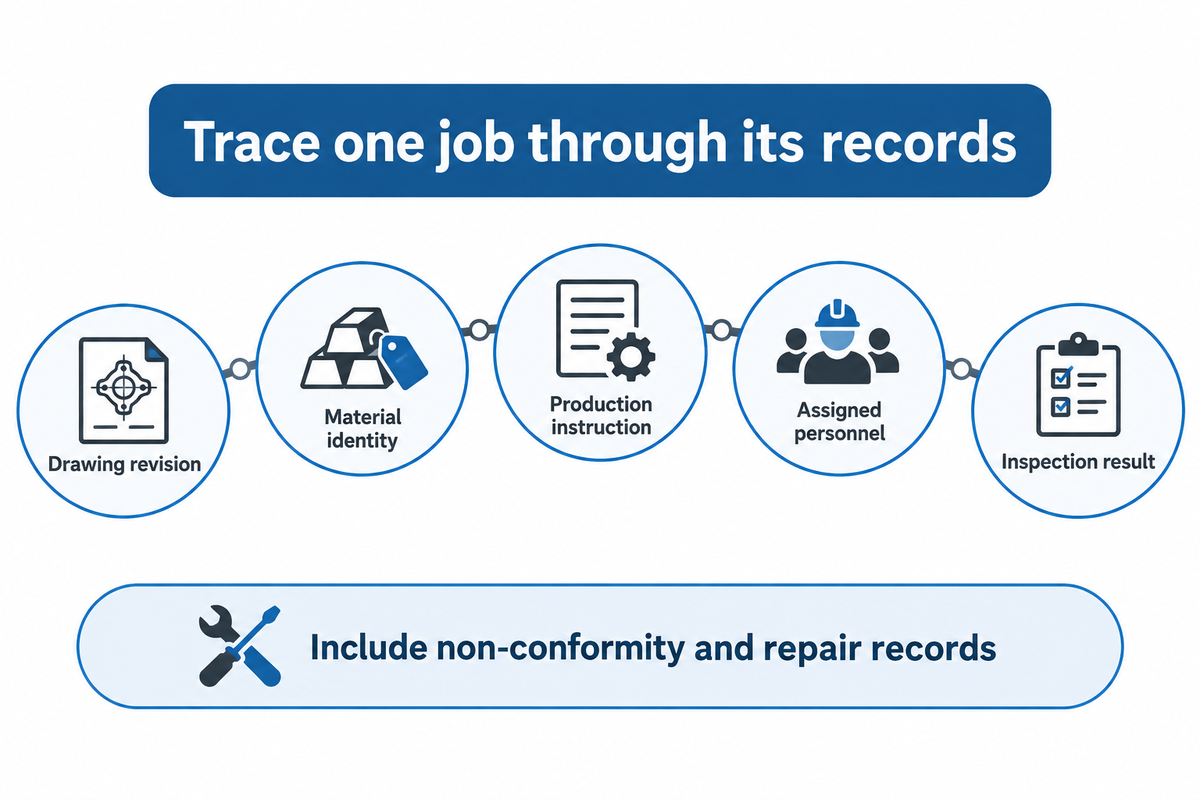
A good welding quality assurance plan ties the revision of the drawing to the identification of the material, the production instruction, the assigned personnel and the inspection result. The welding quality control plan specifies the required checks and release responsibilities. Focus on a single joint in the chain during a document review and a gap will be easier to find than in a folder organized only by document type.
Include in the same trail the non-conformity disposition and any required repair inspection. Upstream preparation matters too. Beveling of plates for heavy fabrications should serve the joint preparation, not define it.
ISO 3834 certification cost and lead time
Budgeting for certification has two parts: getting the manufacturing operation ready and paying for assessment and continuing certification activities. The preparation work may include procedure qualification, personnel development and corrective actions. Quotes vary, so compare providers against the same manufacturing request for proposal. The auditor should be given a clear description of operations to be assessed.
TWI’s certification guidance states that elements which affect the quotation include the size and location of the operations and existing certification. For finance, the audit fee should be kept separate from the cost of closing technical gaps. Comparing the costs should include the terms and conditions of continuing surveillance.
- Define the scope: identify the entity, sites, product range and required quality level.
- Close preparation gaps: assign procedures, qualifications, production controls and document responsibilities.
- Demonstrate implementation: assemble records showing the controls working on applicable jobs.
- Complete the assessment process: resolve findings and agree the ongoing scheme obligations.
Hypothetical example: Finance approves a certification quotation while Production plans to introduce a different welding process. The certification quotation is just one budget item. The coordinator first checks the welding process against procedure and personnel coverage and identifies the work required to prepare the scope. The purchasing department separates that work from the certifier’s fee and travel costs. The project schedule follows the outstanding technical tasks and the provider’s availability, instead of treating the audit date as the start of implementation. This approach provides Finance with a listed set of dependencies, and allows the plant manager to explain why a low audit price doesn’t mean that the total preparation cost will also be low.
ISO 3834 certification bodies and certificate scope
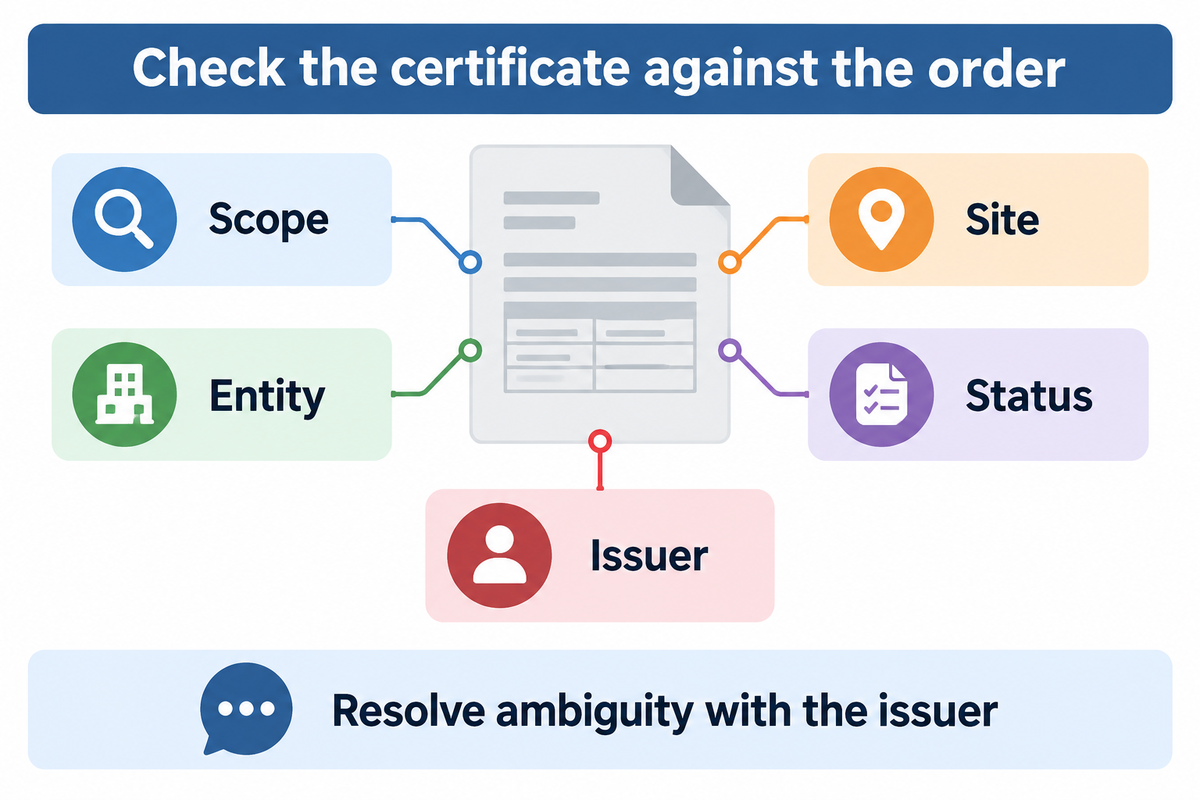
A certification evaluates the welding scope provided by a manufacturer. Buyers should review the certificates against the purchase order for the scope, entities, sites, status and issuer. Where accredited certification is required, confirm the scope covered by the accreditation; a logo or membership doesn’t verify the requirement.
El International Institute of Welding’s manufacturer certification scheme indicates that, under the standard, certification is optional. Contractual requirements may oblige parties to seek third-party certification. IIW also links to a register of manufacturers certified by its scheme.
The scope of a certificate should define the manufacturing work covered. Ambiguity should be resolved by the issuer. It should identify the legal entity and location doing the work. It’s evidence of the work covered by its stated scope, not automatically of other work at the same site or another site.
Surveillance and reassessment are handled in accordance with the specified scheme. TWI’s notice on maintaining certification identifies changes that should be reported, e.g. equipment, location and welding-coordination changes. When reviewing procurement, the current state of operations should be considered, as well as the printed expiry date of the certificate.
Welding automation for heavy fabrication
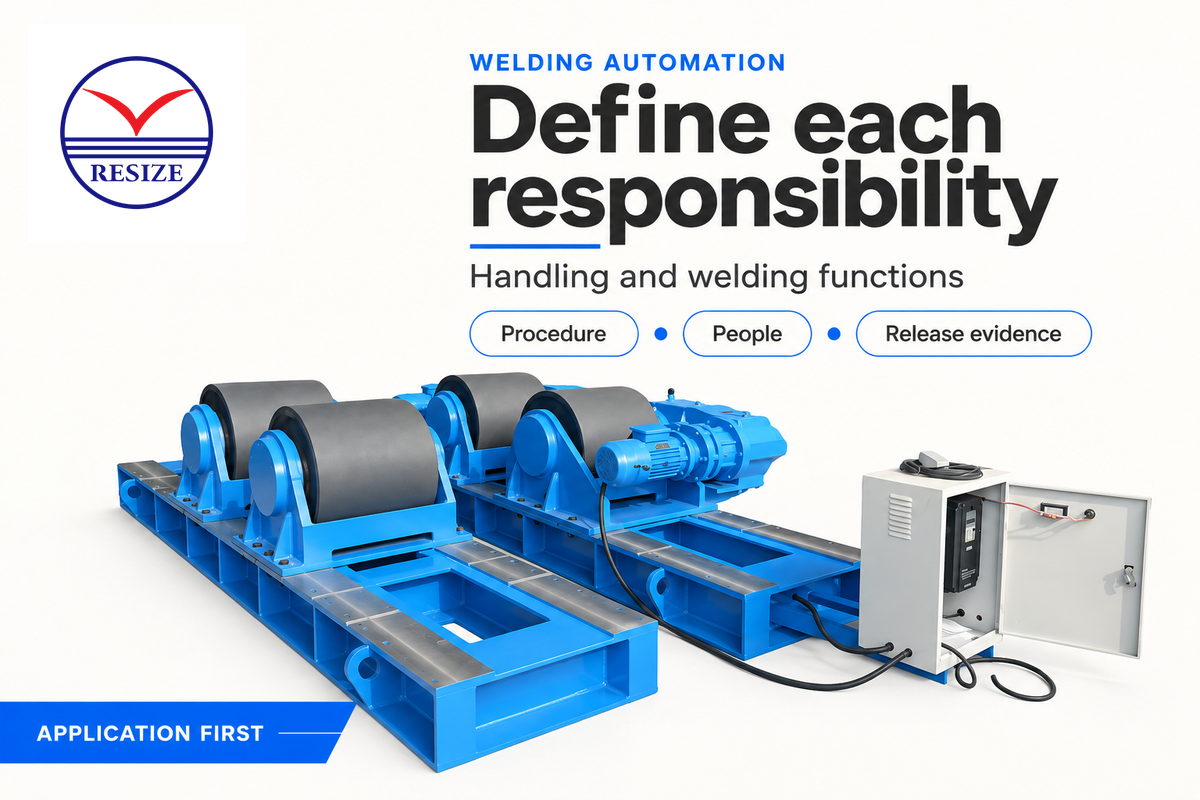
Automation of welding processes changes how a production task is performed; however, the manufacturer still requires a procedure, appropriate personnel, equipment control and release evidence. For heavy fabrication, specify welding and handling functions separately and assign responsibility for each task.
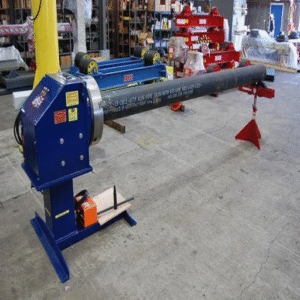
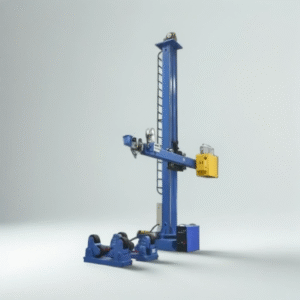
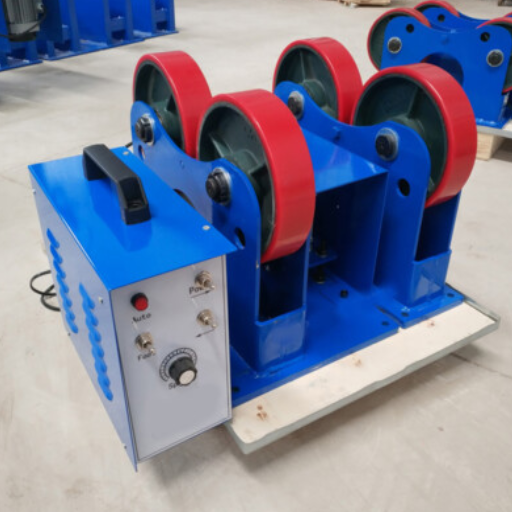
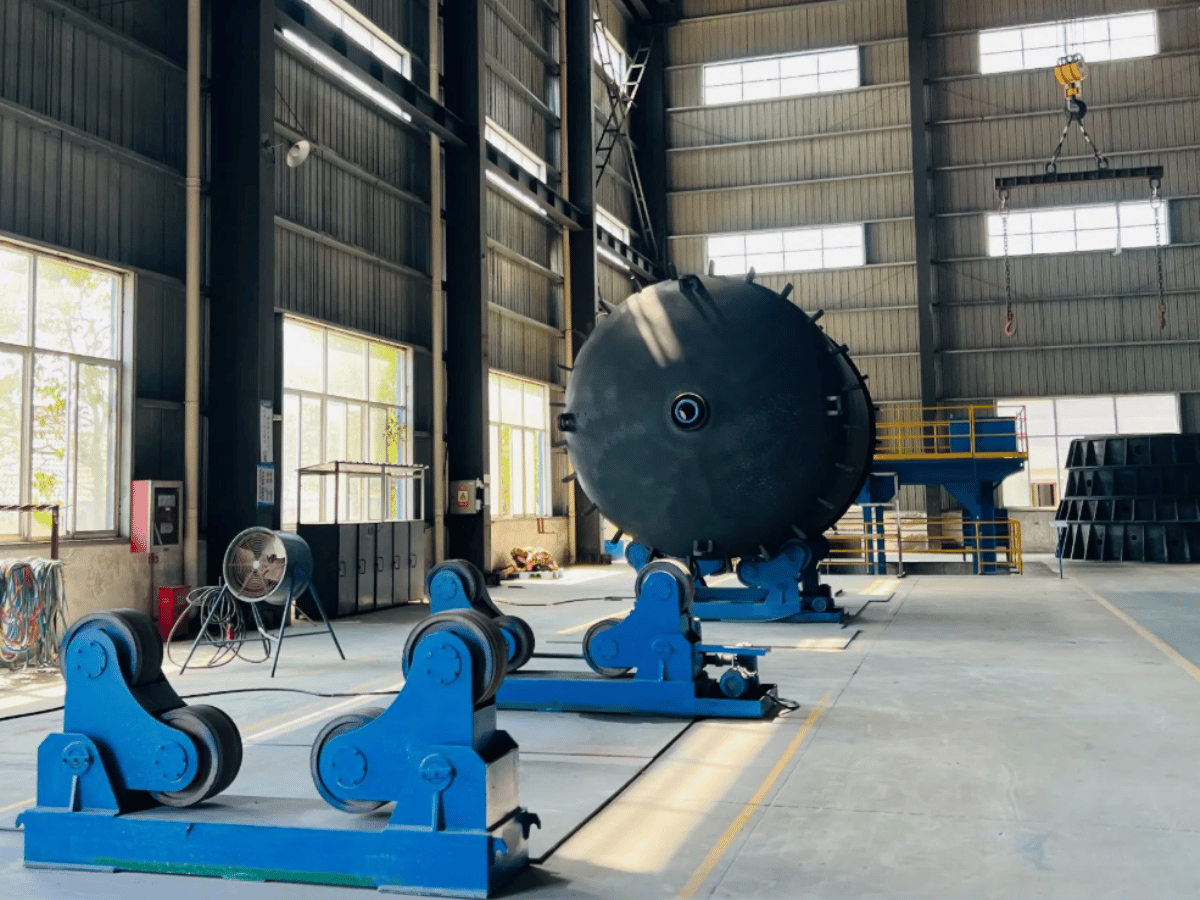
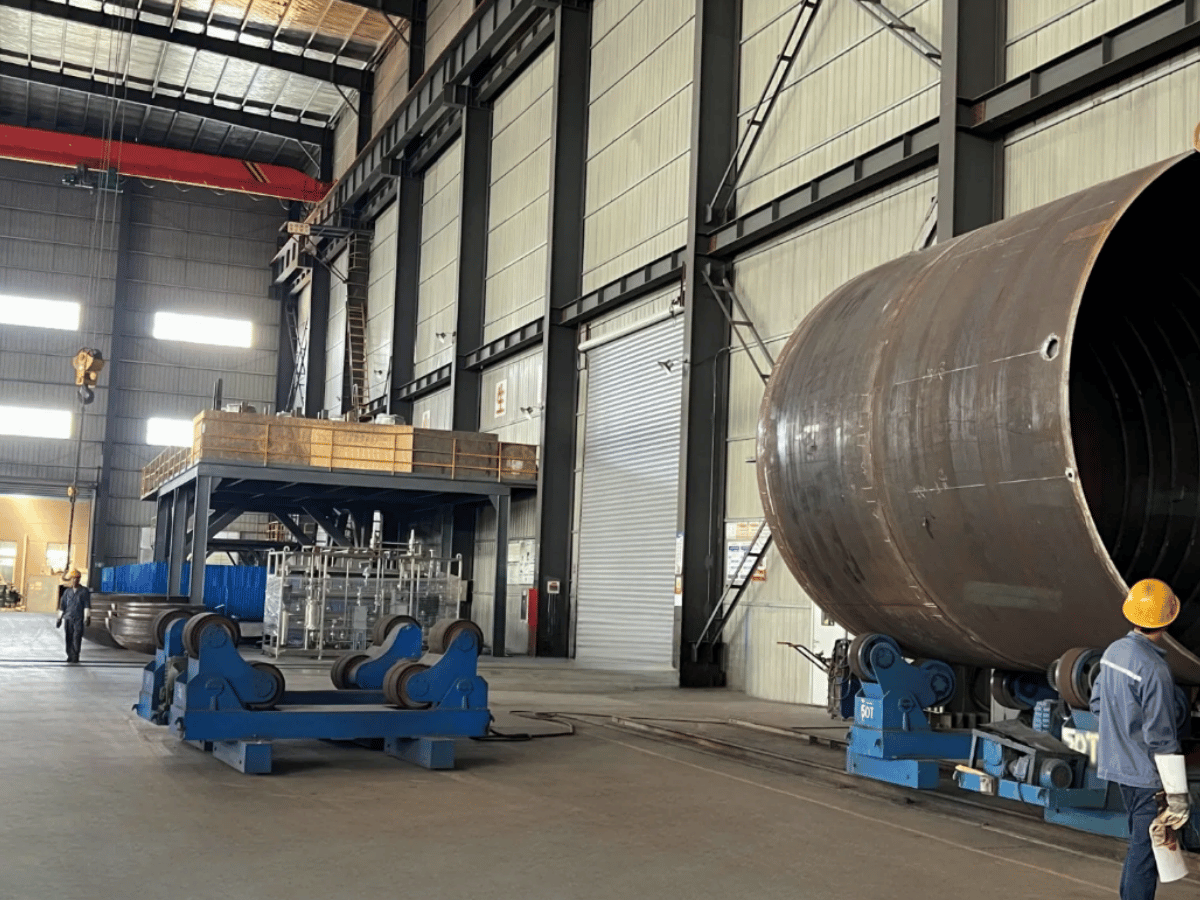
For cylindrical work, welding rotators address workpiece movement; they do not define the welding procedure. Positioning, torch motion and seam tracking in welding each have a place in the production arrangement. An equipment demonstration should use agreed tasks and acceptance criteria pertaining to the application in question.
RESIZE offers wind tower production line equipment. When discussing a line, provide the product range, joints and process requirements, handling requirements, and expected interfaces with the quality system of the plant. The background on the application of welding wind turbine structures can help support that discussion.
A sustainable operational routine requires personnel who can maintain it. For welding manufacturing teams, time should be allotted for inspection, records and technical queries in addition to production. Equipment capability and management of welding should be reviewed jointly before making the decision that a given cell is ready for routine production.
Industry Outlook: ISO 3834-2:2021 and current supporting standards
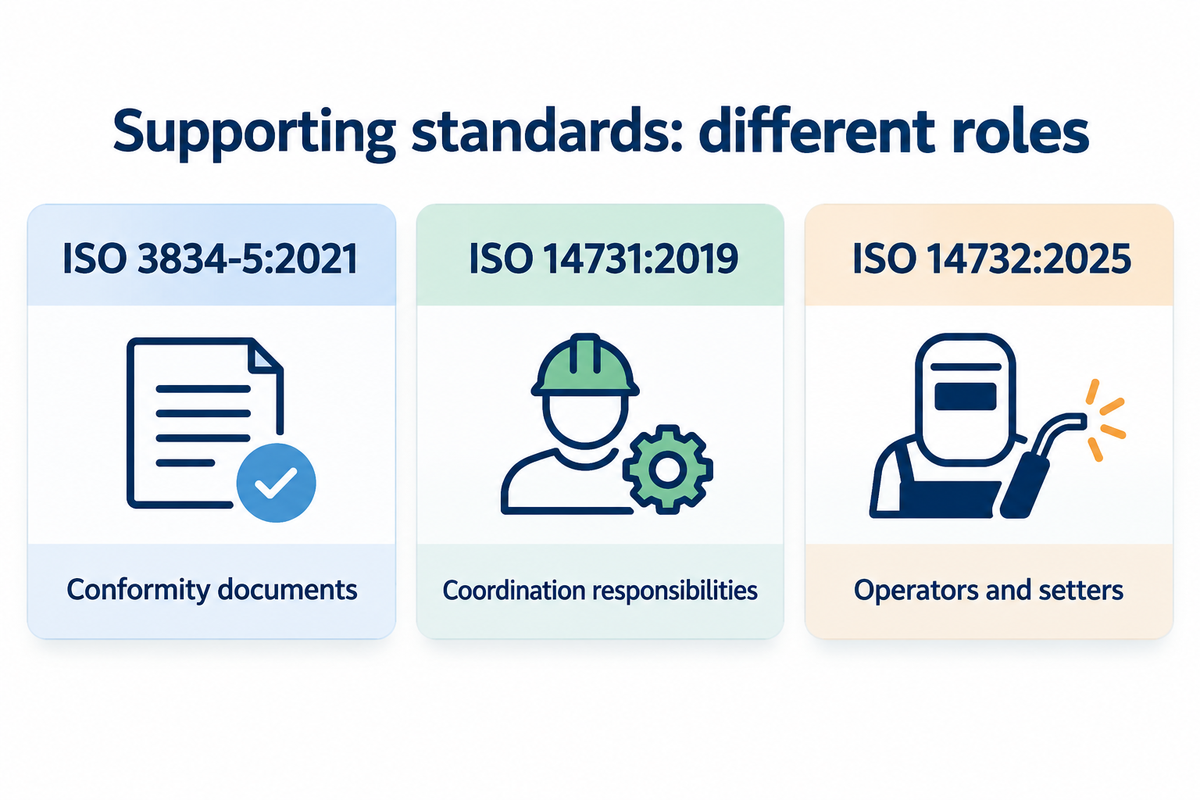
Standards updates make document control a practical purchasing issue. A quote can name the right standard family while still using an old supporting document. Prior to a new project, make sure the contract, procedure references and personnel requirements are aligned with the editions that will apply to that work, including any transitional arrangements.
ISO 3834-2:2021 remains current following confirmation on 22 September 2026. Confirmation retains the existing edition; it does not create an ISO 3834-2:2026 edition. ISO 3834-6:2024 provides implementation guidance without adding requirements to Parts 1 through 5.
| Document | Role in the review |
|---|---|
| ISO 3834-5:2021 | Documents and provisions for claiming conformity to Parts 2, 3 or 4. |
| ISO 14731:2019 | Welding-coordination tasks and responsibilities; confirmed in 2024. |
| ISO 14732:2025 | Qualification of operators and setters for mechanized and automatic welding within its scope. |
ISO 9001:2026 was published on 16 September 2026 as the current sixth edition. For this version, ISO has provided advisory notes to indicate what differentiates the publication of this edition from the transition of the existing certification, which is governed by the applicable certification cycle. Do not consider a listing of standard withdrawals as evidence that every certificate issued against the previous edition has been immediately invalidated.
For a project entering production after these updates, identify what edition is documented in each controlled document and define who will resolve any discrepancies. A rigorous review should distinguish ISO documents from their national and regional adoptions, such as the EN ISO versions listed in the contract. Contact the publisher for the real requirements. Catalogue pages provide scope and state the status of a standard, but do not replace the quality standard.
Specify the welding-quality scope before buying the equipment, and assign the people, procedures and records that will demonstrate conformity for the actual job.
Frequently asked questions
Is ISO 3834 a certification for a company or for a person?
ISO 3834 addresses the manufacturer’s welding quality arrangements.
Can we outsource welding coordination?
External welding coordination can be an option under the applicable requirements and certification scheme.
How can one become ISO 3834 certified?
Manufacturers start by defining the scope and quality level, then implement the relevant controls before assessment.
What are the benefits of ISO 3834 for businesses?
ISO 3834 gives manufacturers a structured basis for managing welding quality and demonstrating controls to customers.
Who can be our responsible welding coordinator?
The coordinator needs competence appropriate to the allocated welding tasks and the manufacturer’s work.
Where can I get the current ISO 3834-2 standard?
Obtain the standard from ISO or an authorized national standards publisher.
What sectors are covered by EN 3834 certification?
EN ISO 3834 can apply to manufacturers of welded metal products across several industries.
Planning a heavy-fabrication welding line?
Bring your product scope, handling requirements and production interfaces to the equipment discussion. RESIZE can discuss the equipment configuration while your responsible welding personnel establish the applicable procedure and quality requirements.
Related reading
- Robotic welding positioner integration
- Column and boom welding manipulator sizing
- Turning rolls for tank and vessel welding
- Used welding positioner buying checks
Referencias y fuentes
- ISO 3834-2:2021: scope and current status
- ISO 3834-1:2021: selection criteria
- ISO 3834-5:2021: supporting conformity documents
- ISO 3834-6:2024: implementation guidance
- ISO 14731:2019: welding coordination
- ISO 14732:2025: welding operators and setters
- ISO 9001:2026: quality management systems
- IIW: manufacturer certification scheme
- TWI: welding-quality controls
- TWI: certification process and quotation factors
- TWI Certification: maintaining compliance